OTAR® and the Circular Economy: Nitrogen as a Resource, Not a Waste

OTAR® and the Circular Economy: Nitrogen as a Resource, Not a Waste

The fertilizer industry consumes more than 115 million metric tons of nitrogen every year, almost all of it fixed from atmospheric nitrogen using enormous quantities of fossil energy. Meanwhile, waste streams around the world discharge reactive nitrogen to rivers, groundwater and the atmosphere. OTAR® sits at the intersection of these two facts.

The circular economy is well understood in the context of materials and plastics. Its application to nitrogen — one of the planet’s most critical and most wasted resources — is less familiar but arguably more consequential.

The Nitrogen Problem at Scale

The Haber-Bosch process fixes atmospheric nitrogen into reactive ammonia for fertilizer production. It consumes approximately 1–2% of the world’s annual energy supply and accounts for around 1.4% of global CO₂ emissions. Despite this investment, much of the nitrogen fixed by Haber-Bosch is lost before it delivers its intended benefit: leached into waterways causing eutrophication, volatilized to the atmosphere contributing to indirect greenhouse gas emissions through nitrous oxide formation, or discharged in waste streams as a compliance problem.
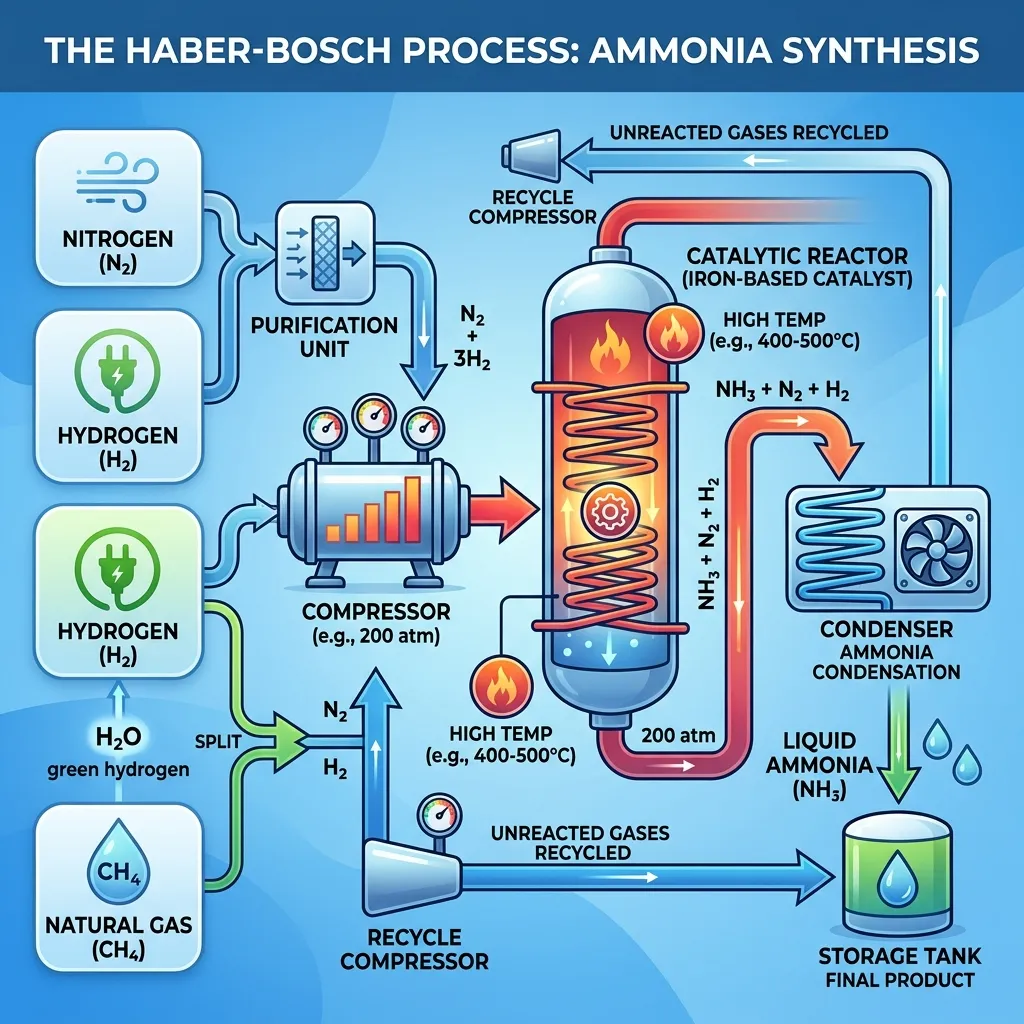
haber bosch ammonia process

What OTAR Does for the Nitrogen Cycle

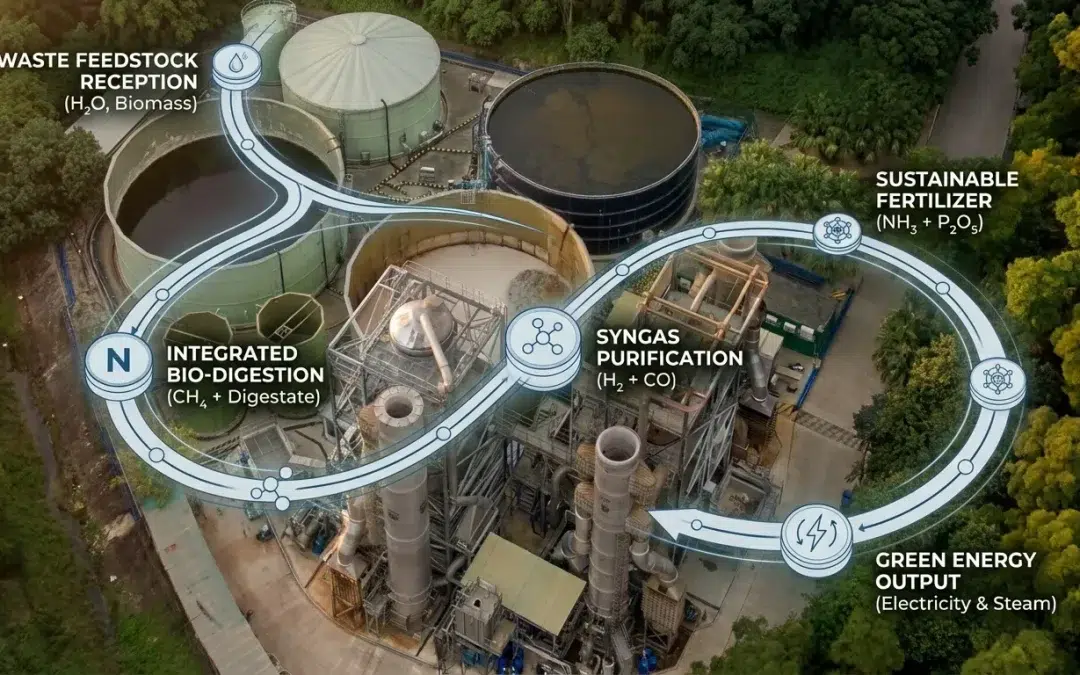
OTAR® intercepts reactive nitrogen at the point of concentration — in digestate, wastewater, leachate or industrial effluent — and returns it to productive use as ammonium hydroxide, anhydrous ammonia or, in Variant 3, ammonium sulfate. This closes a loop that is currently open: rather than fixing new nitrogen from the atmosphere (at Haber-Bosch energy cost), OTAR® captures nitrogen that has already been fixed and would otherwise be lost. The environmental arithmetic is compelling: every metric ton of nitrogen recovered by OTAR® displaces approximately 2 metric tons of CO₂ equivalent from avoided Haber-Bosch synthesis.
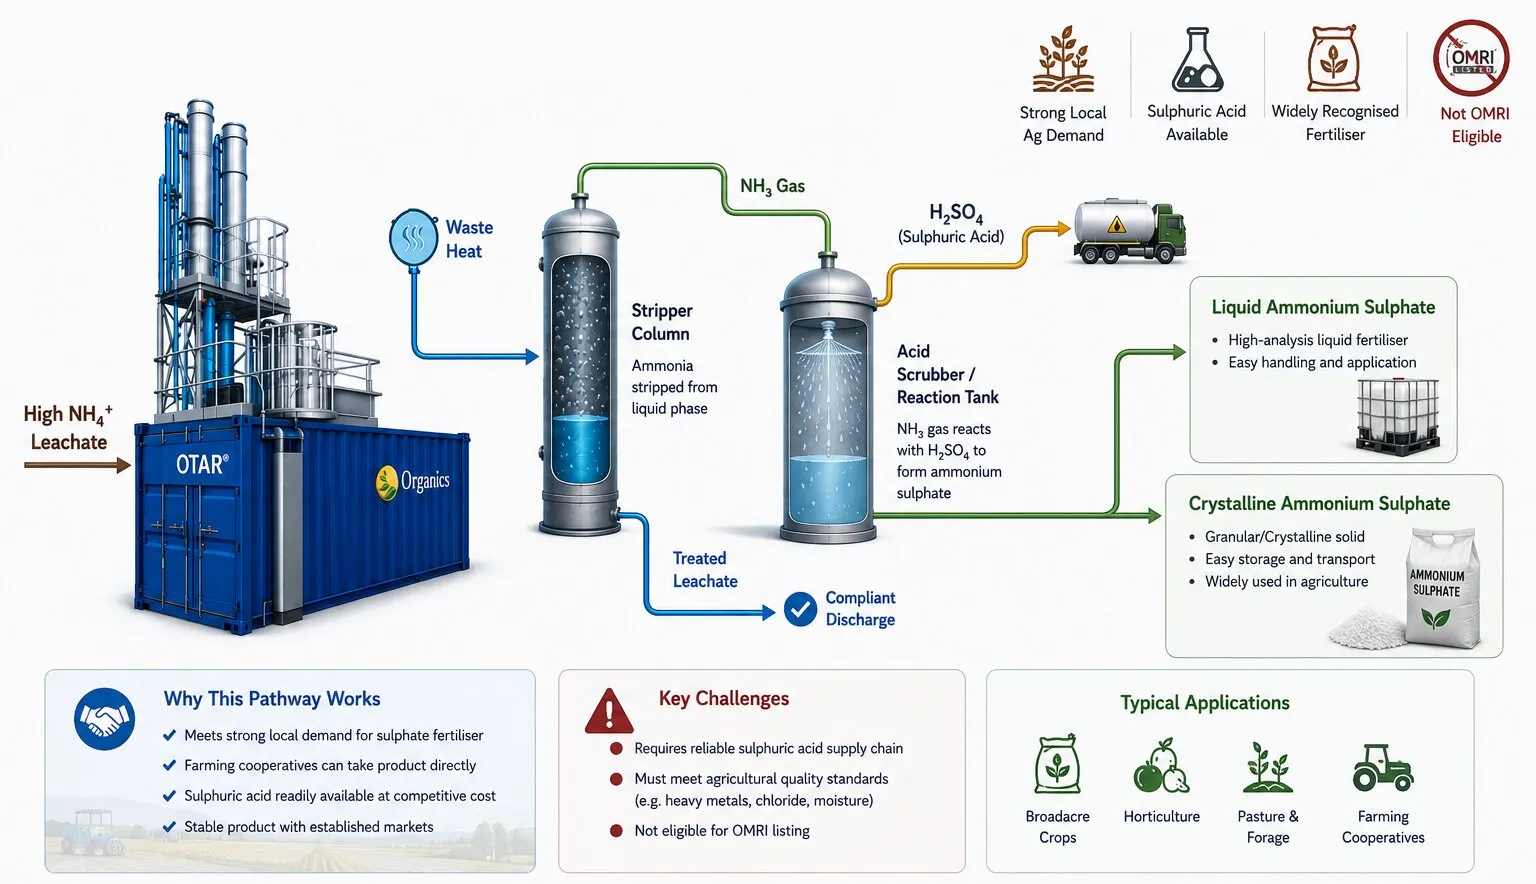
 

OTAR var3

Regulatory and Policy Tailwinds

In the United States, nitrogen is already regulated through Clean Water Act NPDES permits, state nutrient criteria and total maximum daily load (TMDL) programs. Beyond individual permits, the Mississippi River/Gulf of Mexico Hypoxia Task Force has set targets to cut nitrogen and phosphorus loads to the Gulf by 20% by 2025 and 45% by 2035, and the states in the basin have written nutrient reduction strategies that reach wastewater plants, industry and agriculture. Programs such as the Chesapeake Bay TMDL apply the same pressure in other watersheds. OTAR® operators are positioned ahead of these trends — recovering nitrogen today, before tighter limits and nutrient-use expectations reach their sites.

The Hydrogen Economy Dimension

Ammonia is increasingly recognized as a scalable carrier for renewable hydrogen — its high energy density and existing global transport infrastructure make it a leading candidate for zero-carbon maritime fuel and industrial energy storage. The U.S. already has ammonia storage, pipeline and terminal infrastructure serving agriculture and industry.

OTAR® Variant 2 can produce anhydrous ammonia (by concentration of recovered ammonium hydroxide) that feeds directly into this emerging value chain. For facilities that invest in OTAR® today as a wastewater treatment solution, the option to supply the hydrogen economy in the future is a genuine strategic asset.
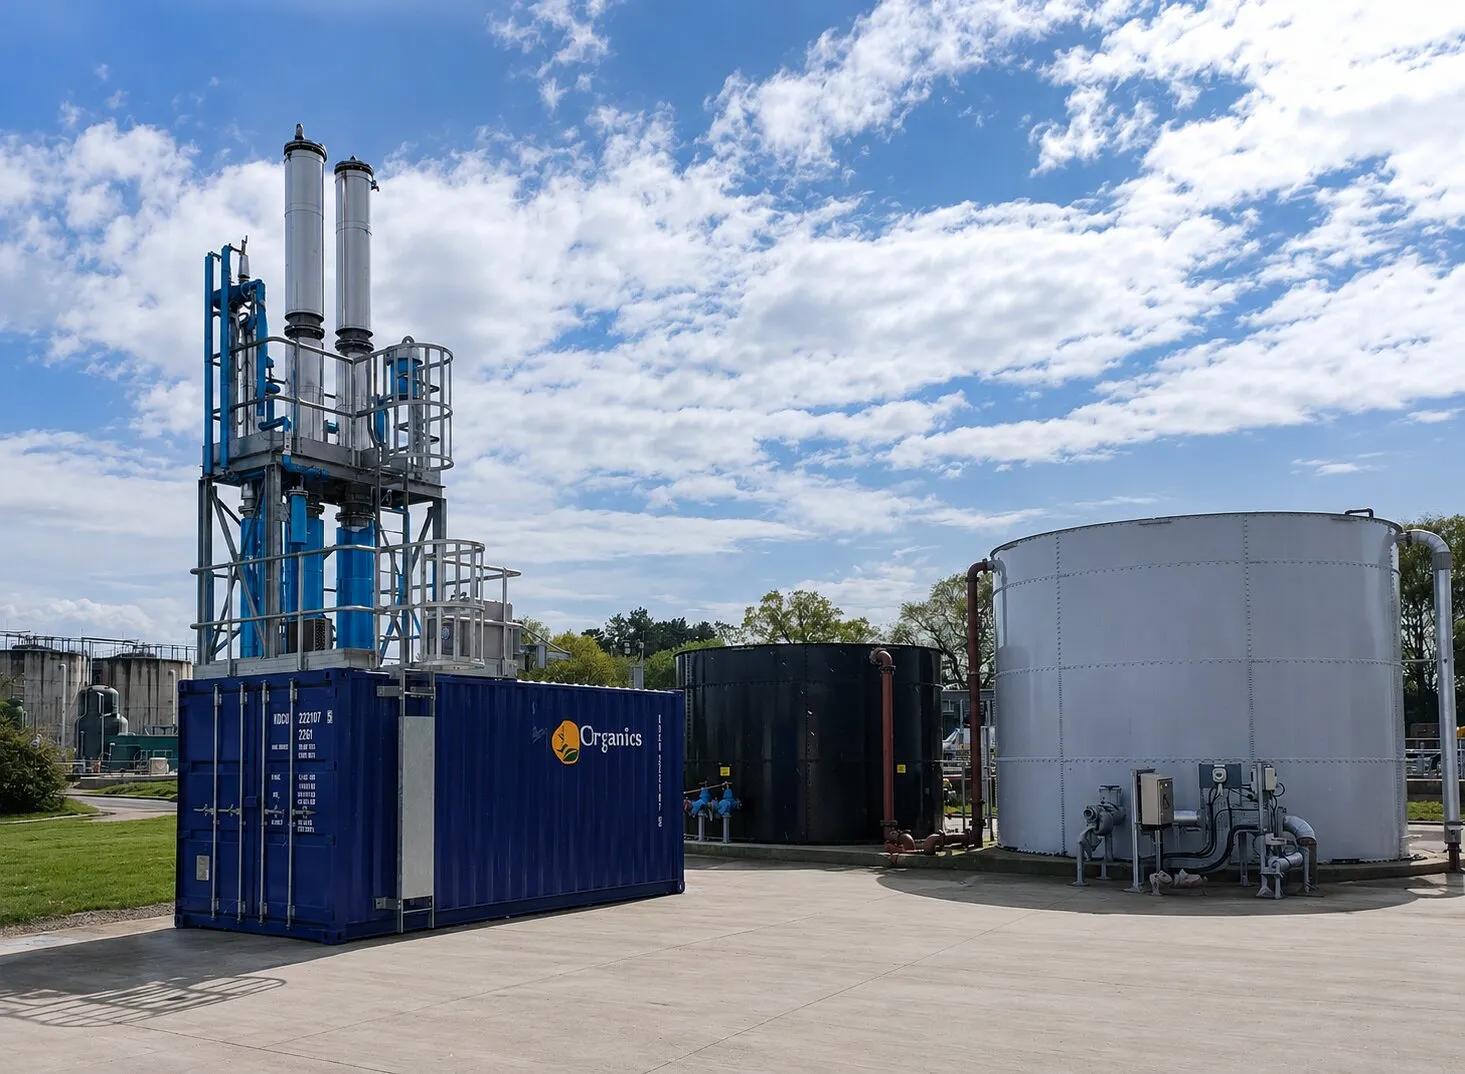
OTAR AD site 2

What This Means for Each U.S. Segment

Recovered nitrogen carries a different strategic value depending on who you are:
planta biogas recuperacion amoniaco webp

Commercial AD & Biogas Developers

Returning nitrogen to productive use strengthens the sustainability story of digestate-derived products and of the renewable-energy project as a whole.
animal farm icon

Large-scale dairy & swine CAFOs

Capturing ammonia before it volatilizes or leaches keeps nitrogen on the farm’s books, supports state nutrient management expectations, and replaces purchased fertilizer.
municipal wastewater

Municipal wastewater treatment plants (WWTPs)

Recovering nitrogen from centrate reframes the plant as a water resource recovery facility, while cutting the energy and nitrous oxide associated with biological nitrogen removal.
gestion residuos organicos recuperacion amoniaco webp

High-protein food & beverage processors

Recovered nitrogen supports corporate ESG and net-zero commitments with a measurable, auditable number, and can close the loop with agricultural suppliers.
Landfill leachate icon

Solid waste & landfill operators

Leachate nitrogen that would otherwise be destroyed biologically can be returned to use, turning a decades-long compliance liability into a documented resource-recovery outcome.
Food and Beverage Processing: The Ammonia Recovery Opportunity

Food and Beverage Processing: The Ammonia Recovery Opportunity

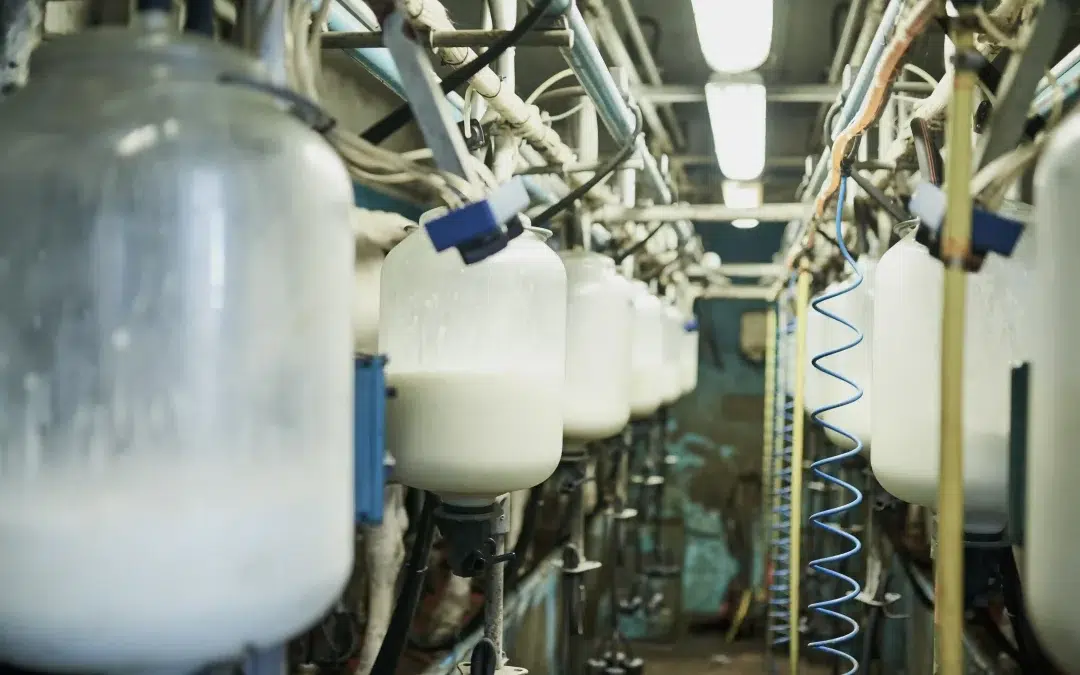
A large dairy processing plant may generate sufficient ammoniacal nitrogen in its effluent to produce 200+ metric tons of ammonium hydroxide per year — a product with industrial, agricultural and OMRI-eligible markets — that it is currently paying to destroy.

High-protein food and beverage manufacturing produces effluents with ammoniacal nitrogen loads that are challenging to treat conventionally — and highly suitable for thermal ammonia recovery.

Sources of Ammonia in Food and Beverage Manufacturing

Ammonia in food processing wastewater arises primarily from protein degradation. Sectors with the most significant loads include:

dairy cow farm6 scaled 1

Dairy Processing

whey, CIP effluents from cheese and butter manufacture

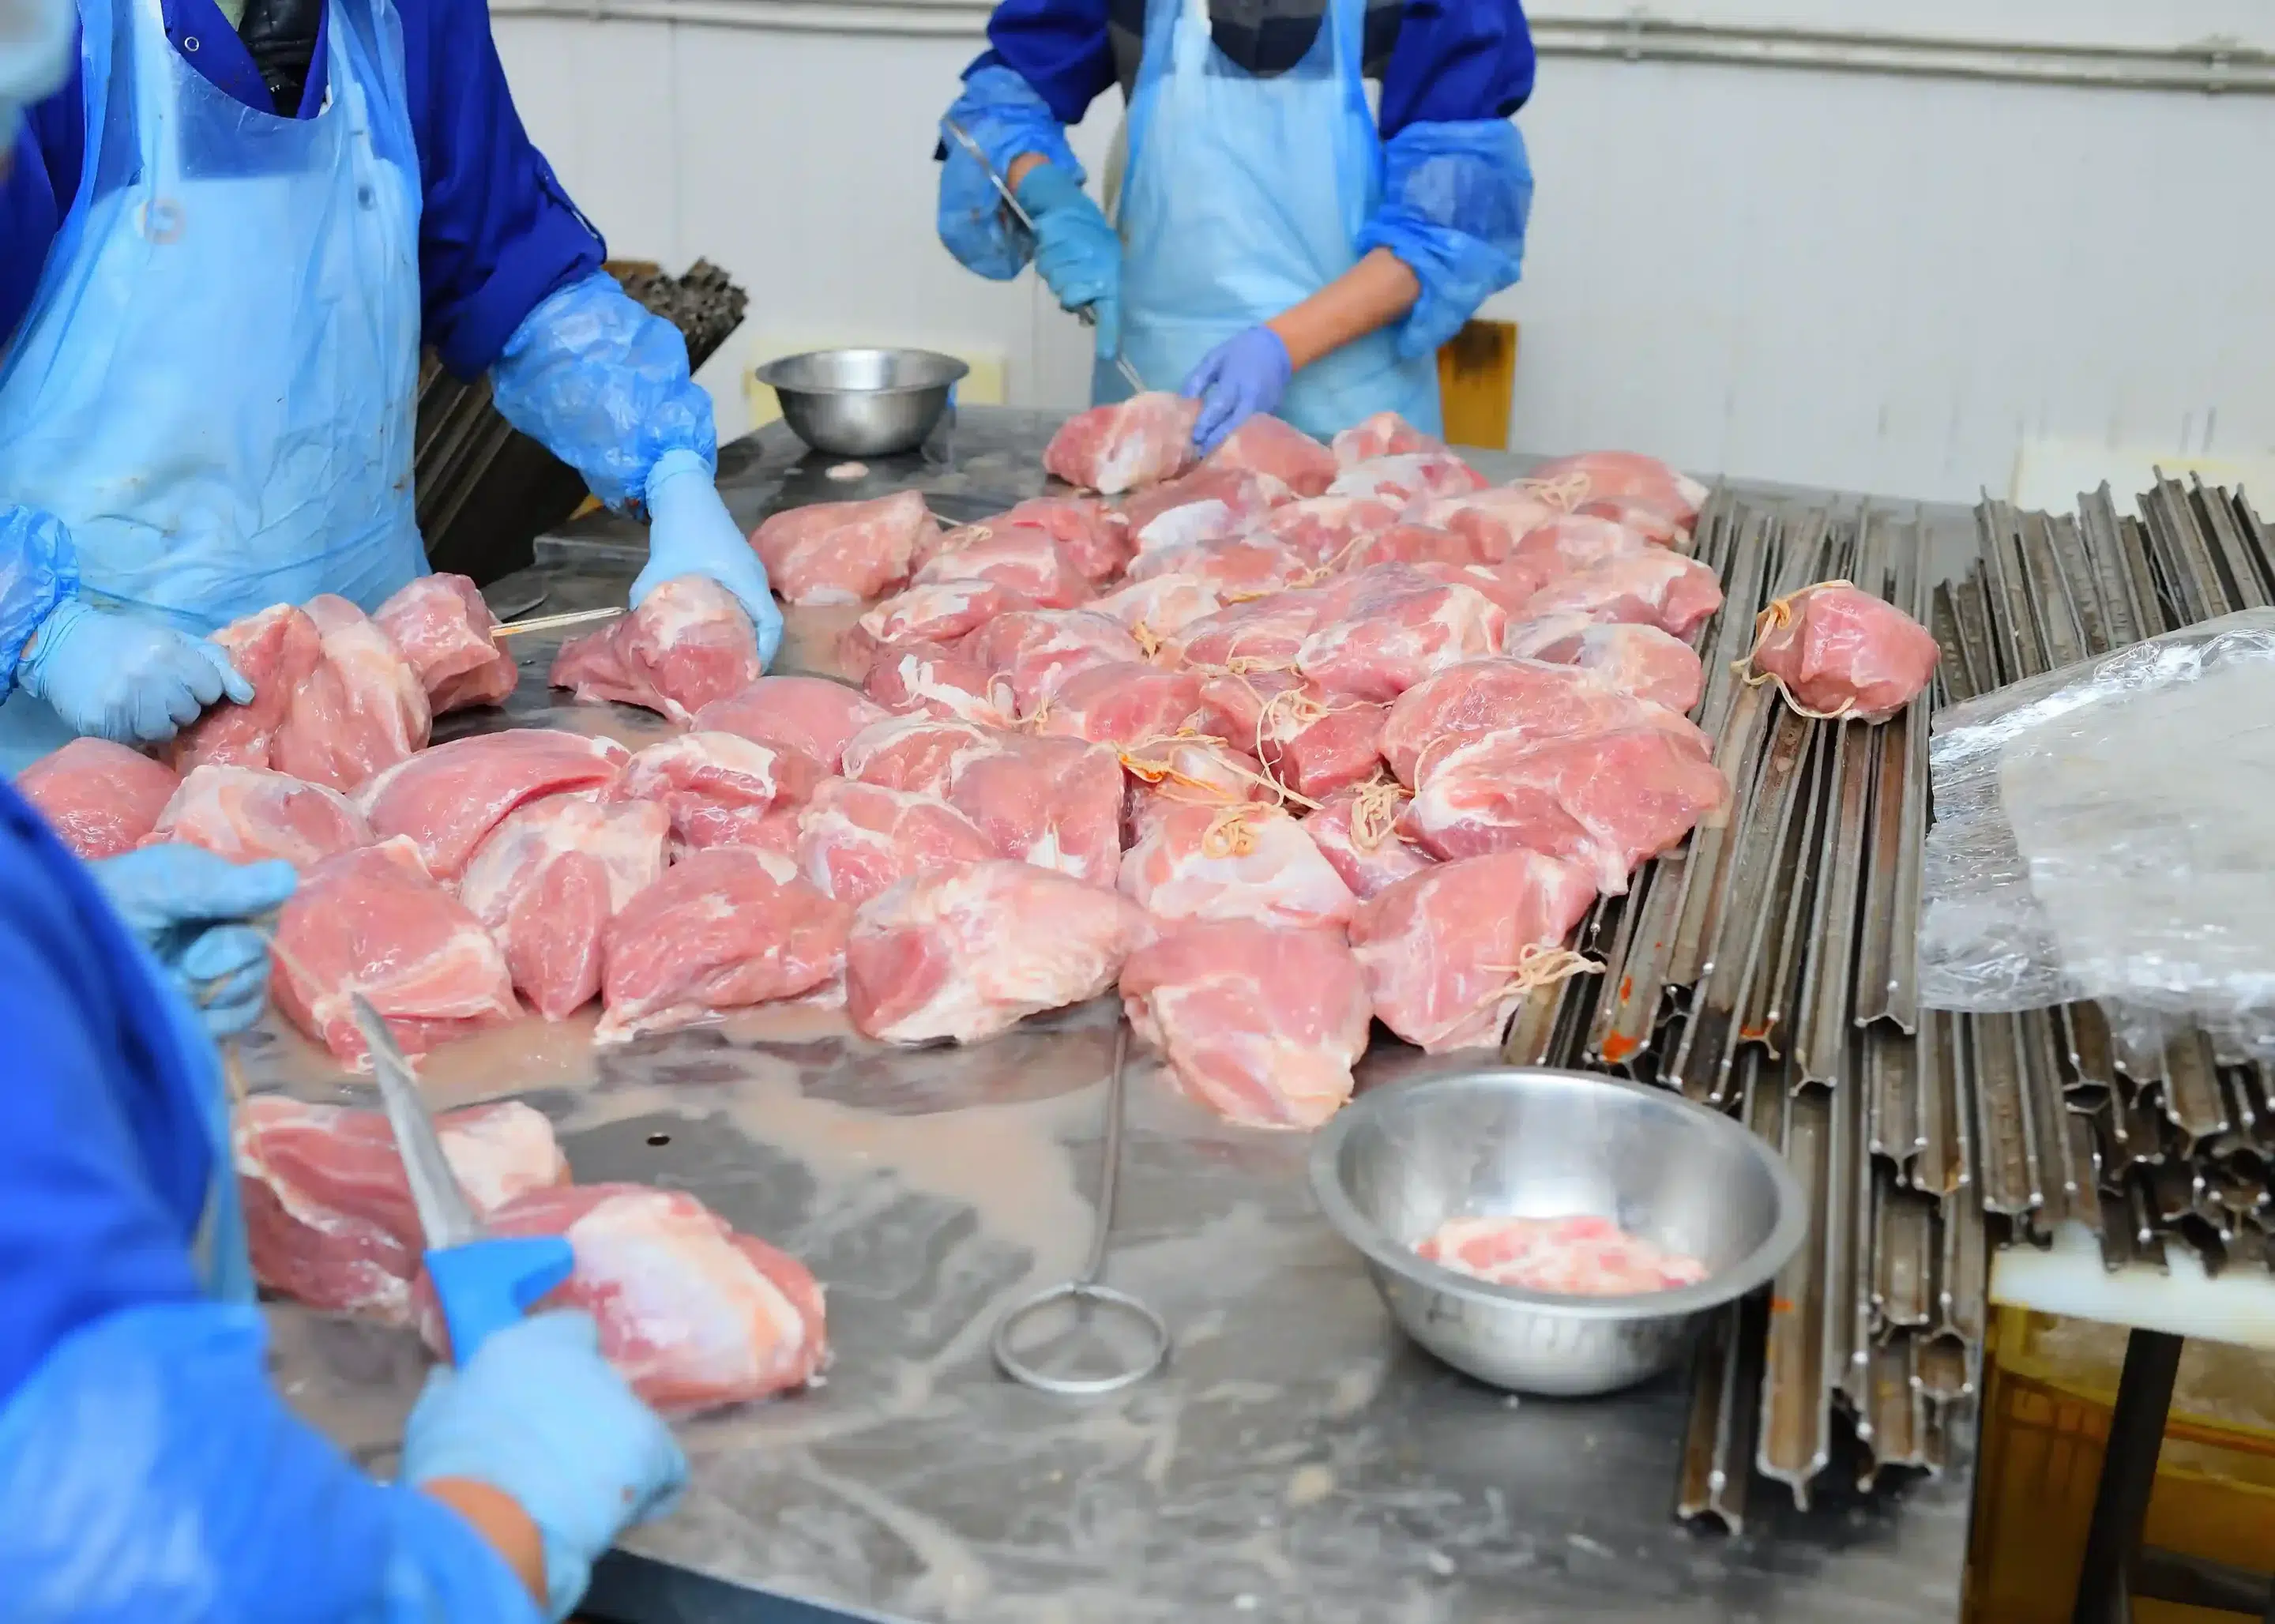
meat processing at a production facility

Meat and Poultry

blood water, rendering condensate, slaughterhouse, and packing plant wash water

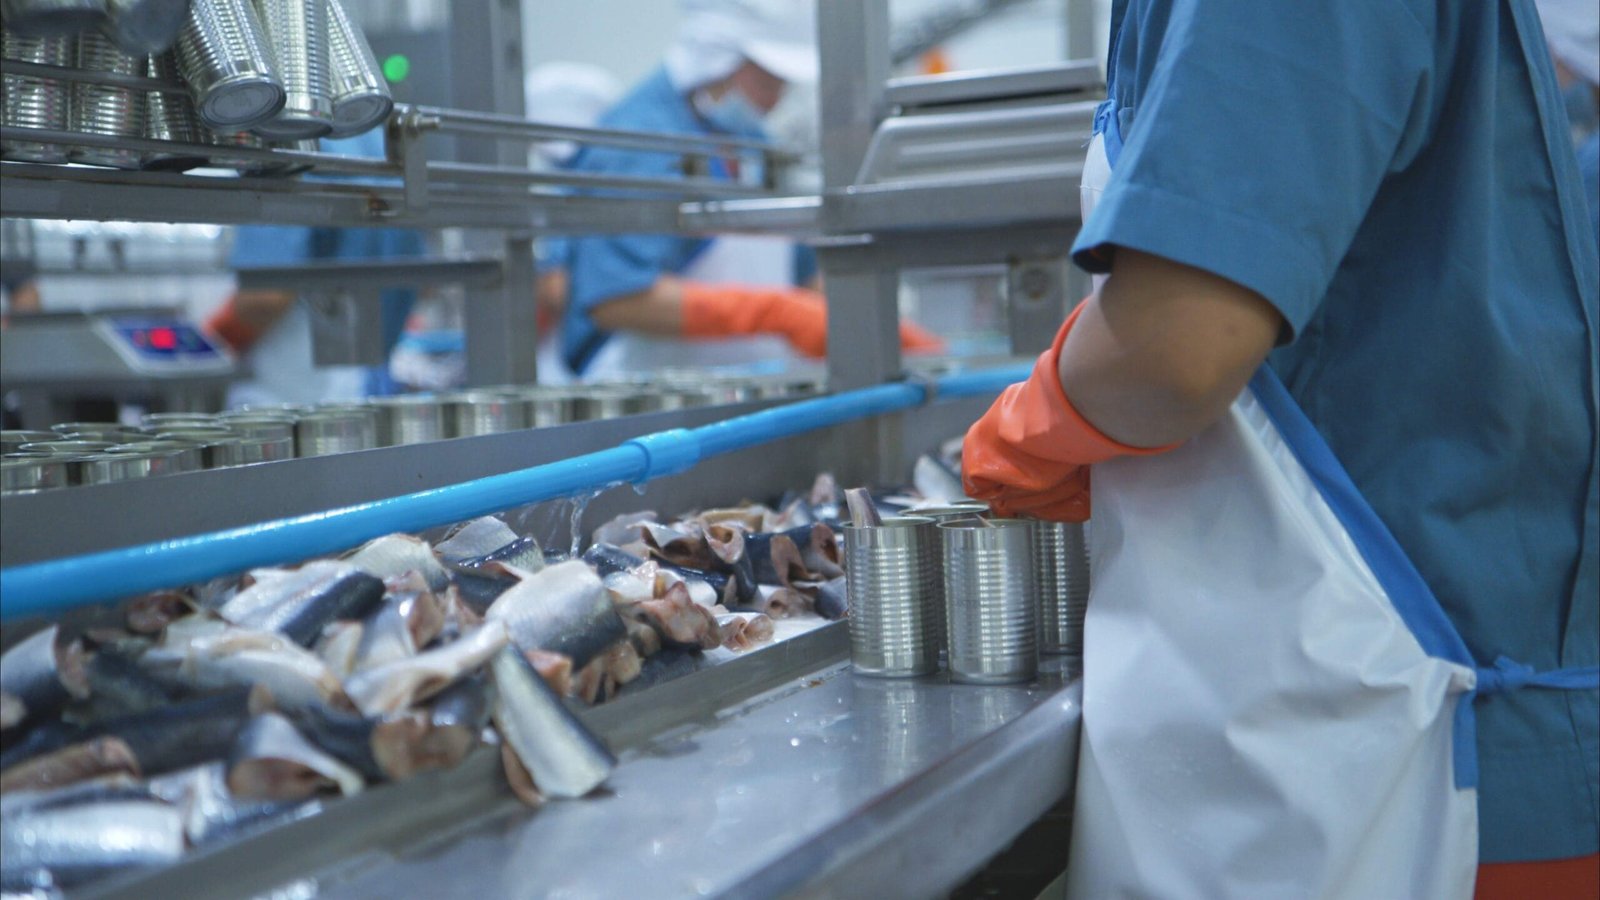
process and production line in canned fish factory 2026 01 07 00 21 07 utc scaled 1

Fish Processing

high-protein wash waters and steam condensates

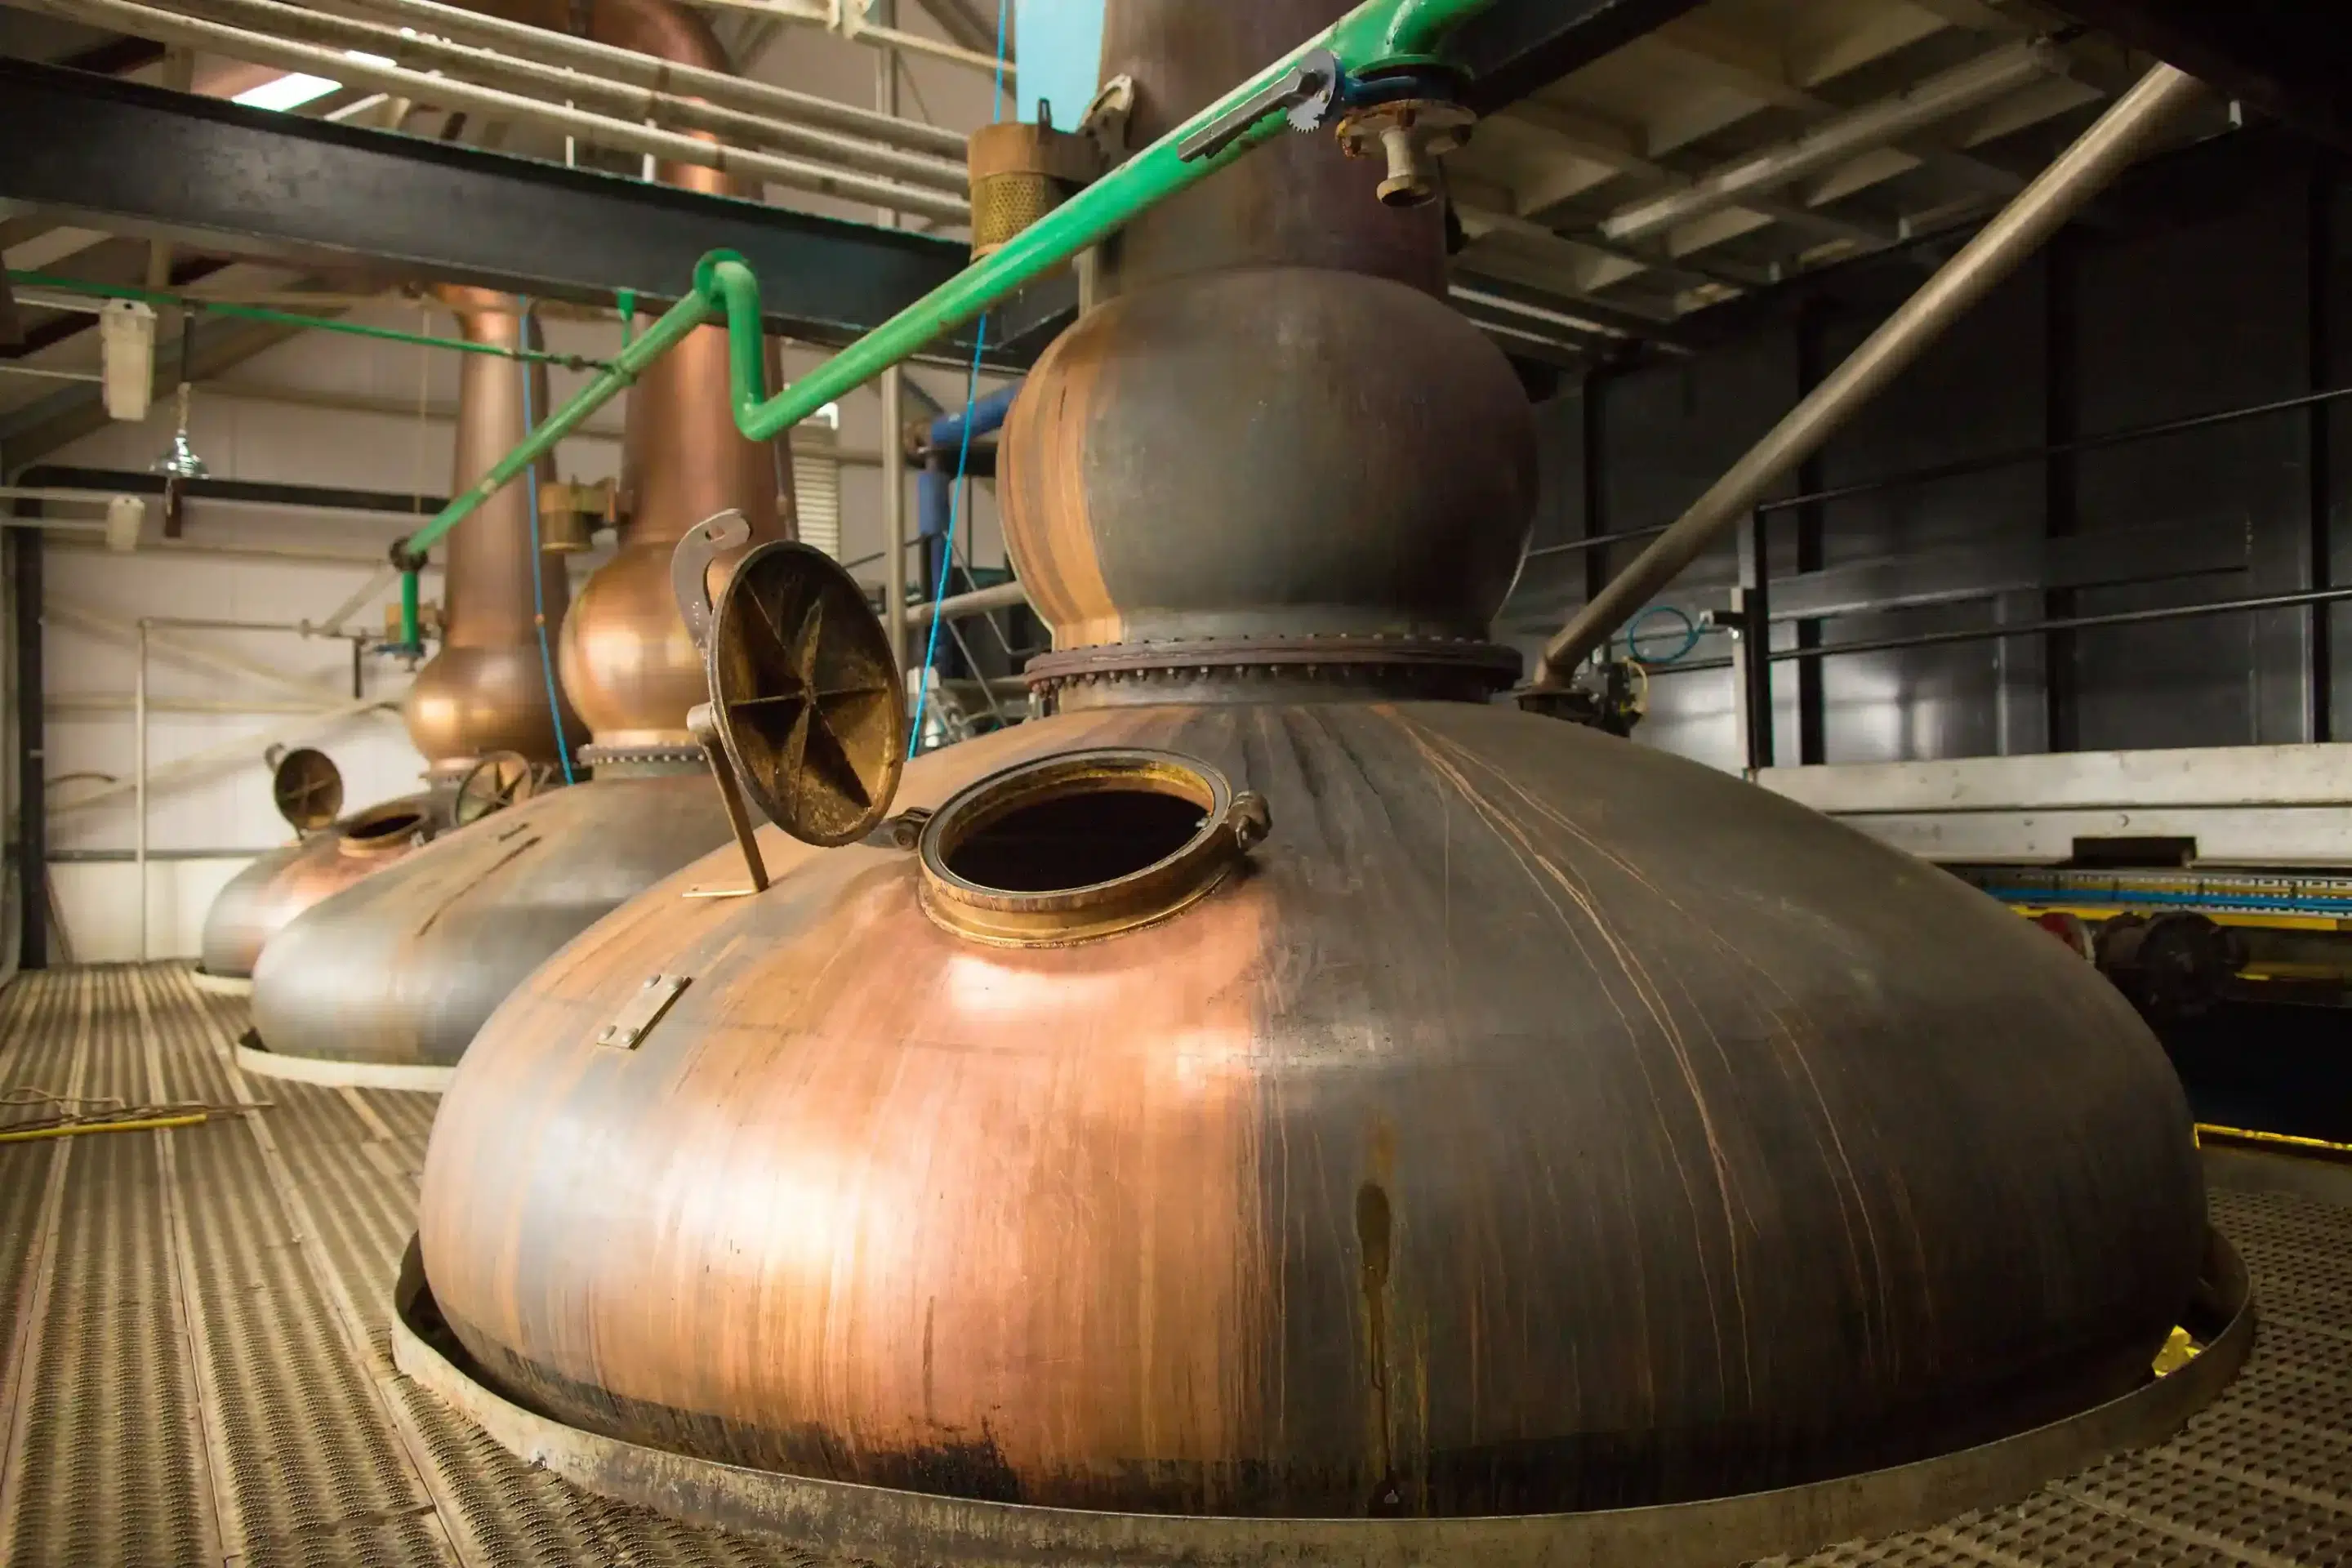
distillery equipment interior still pots in indust

Fermentation, brewing and distilling

yeast effluents, distillery thin stillage

palm oil mill

Vegetable and Starch Processing

blanch water, steep water from protein-rich crops

The Sewer Surcharge Cost Problem

Many food processors discharge to the municipal sewer under an industrial pretreatment permit, and pay surcharges for high-strength wastewater. Ammonia-related strength charges are a growing cost burden — particularly where the receiving treatment plant is itself under nitrogen compliance pressure and passes that cost downstream. Some larger processors face discharge and surcharge costs in the range of $400,000–$675,000 per year, a significant portion of which relates to ammonia load charges.


On-Site Recovery with OTAR

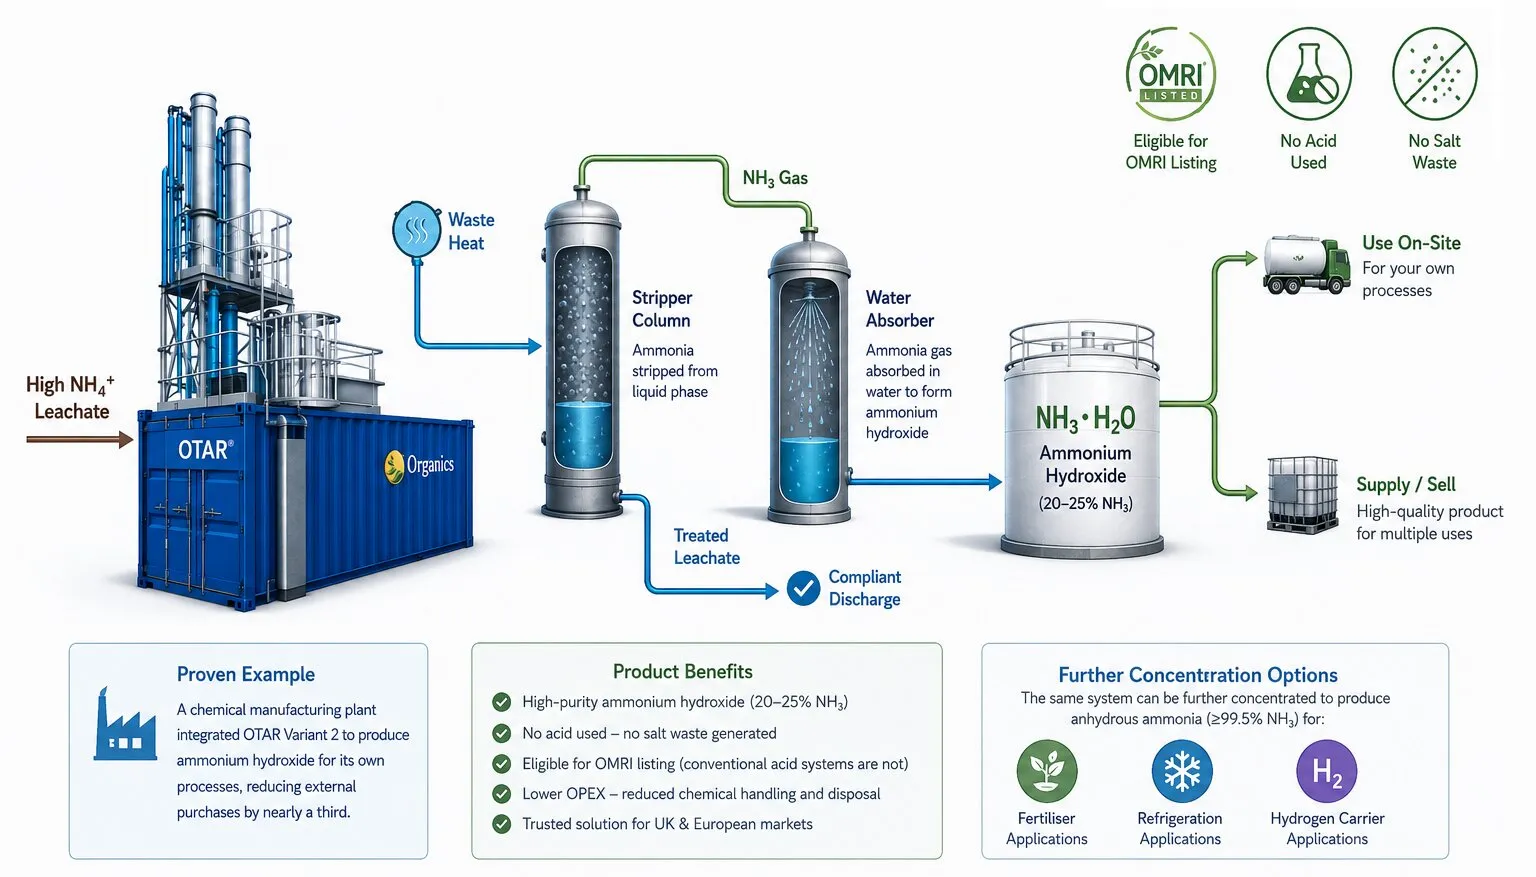
OTAR var2

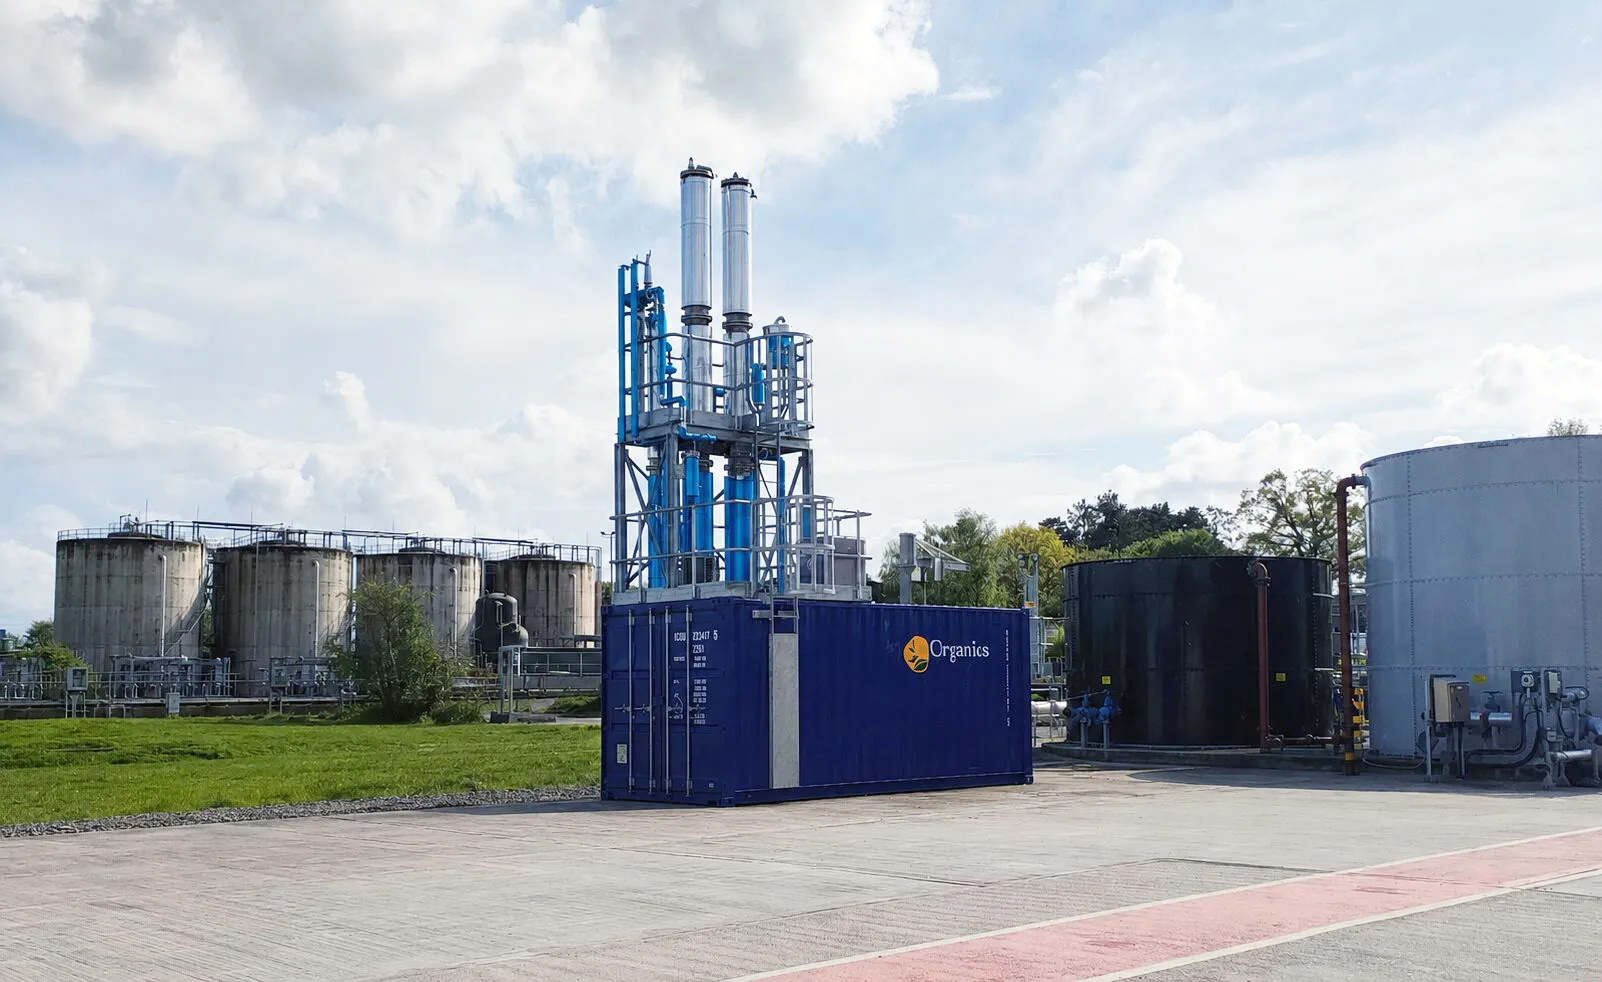
Installing OTAR® on-site allows food processors to capture the nitrogen value before it enters the sewer. OTAR® Variant 2 (water absorption, waste heat driven) is the preferred configuration for most food processing applications: it produces ammonium hydroxide without acid chemistry, making the product eligible for OMRI listing and reducing site safety complexity. Where waste heat from boilers, refrigeration or CHP is available, energy costs are further reduced. For processors with adjacent agricultural relationships, OMRI-listed ammonium hydroxide can be directly applied under the farm’s organic program, creating a closed-loop supply chain within the same business.

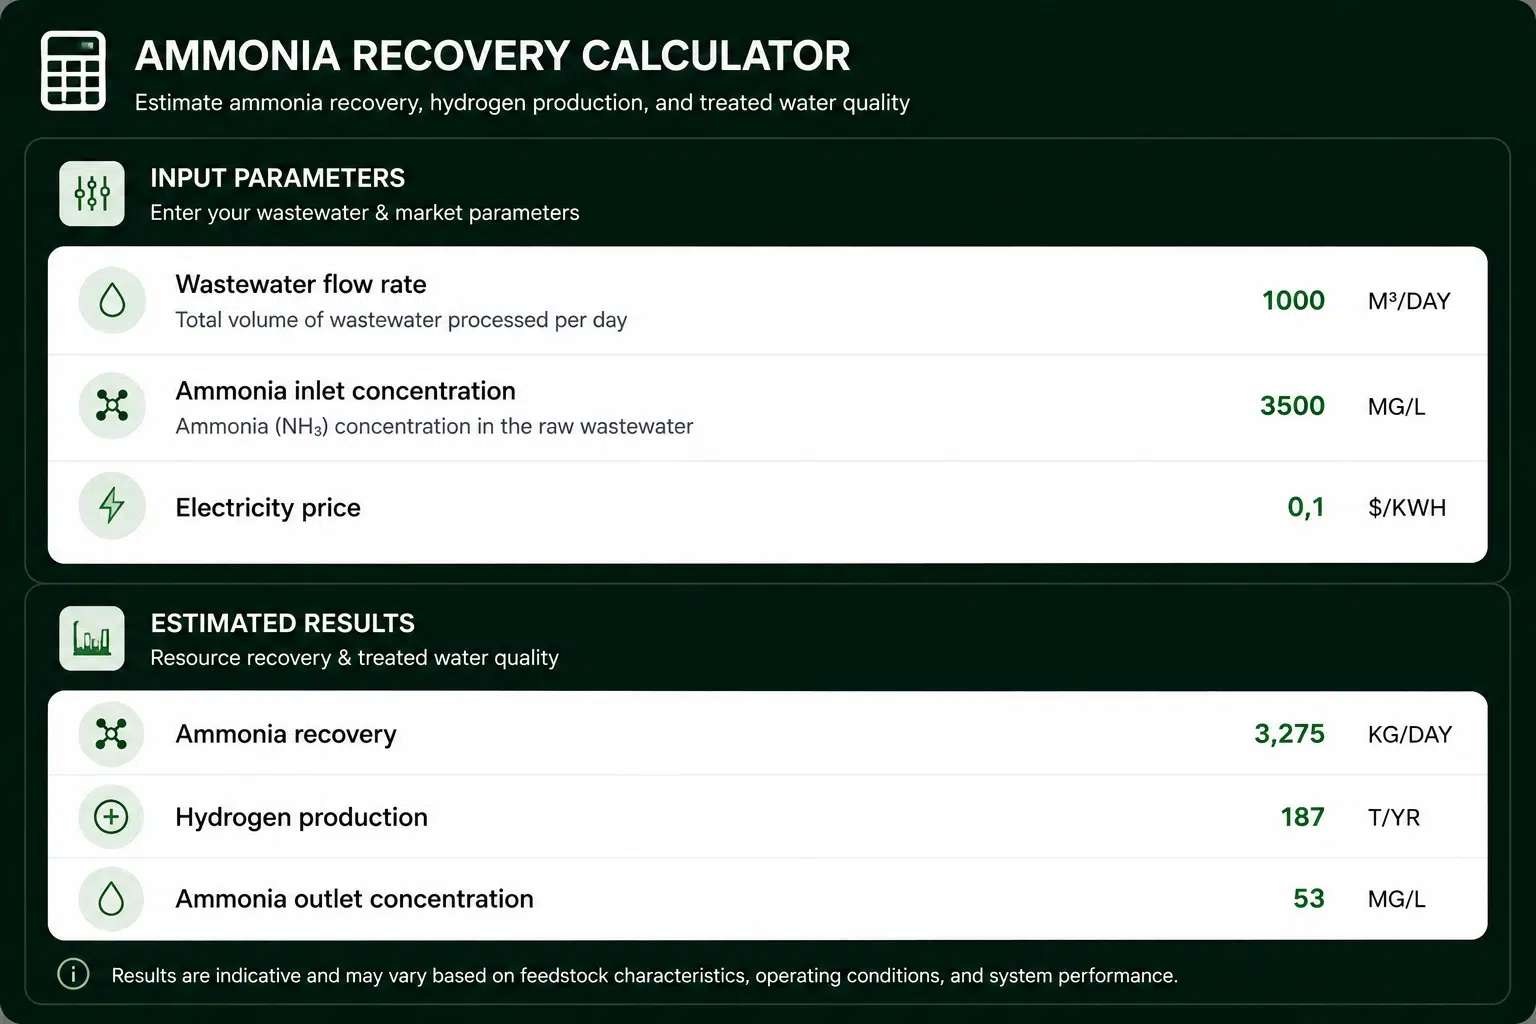
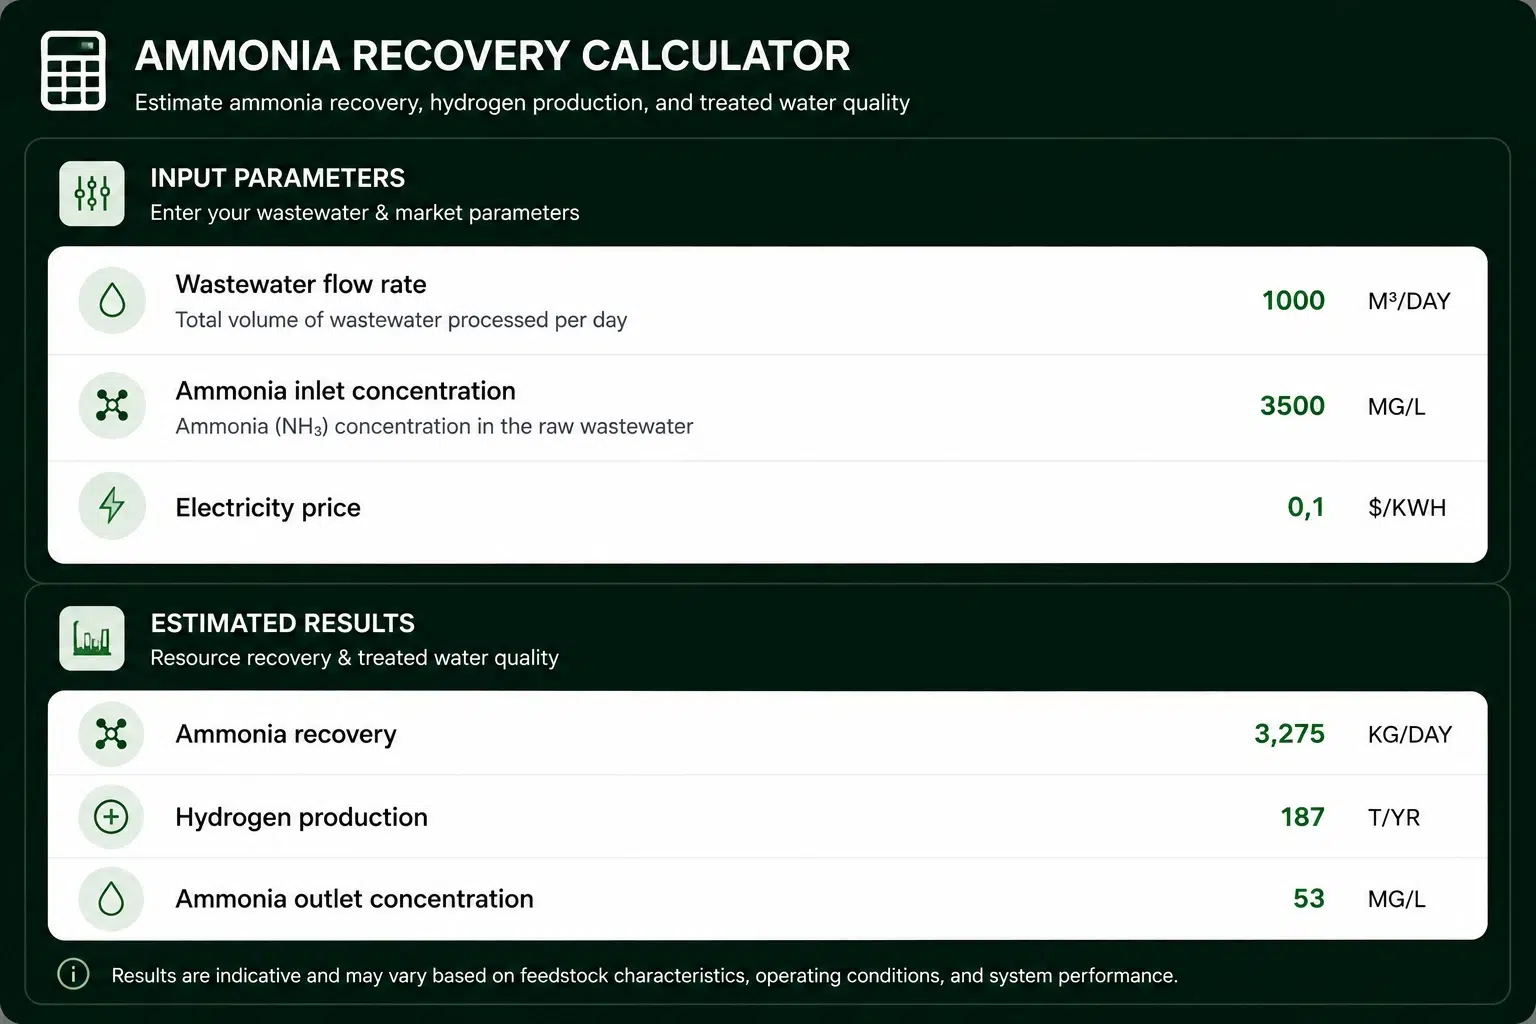
Estimate Your Own Payback

Evaluate the potential to recover ammonia and produce hydrogen while understanding the energy requirements and economics of your wastewater treatment process.

Free • Preliminary Estimate • No Commitment

Integration with Anaerobic Digestion

Many food manufacturers are installing anaerobic digestion to treat food waste and high-strength effluents. AD concentrates ammonia in the digestate reject water, making OTAR® integration at the AD dewatering stage the most efficient point for nitrogen recovery. Organics USA can design integrated AD and OTAR® systems as a combined package, maximizing both biogas yield and nitrogen recovery value from a single organic waste feedstock.

OTAR AD site 2

Where This Fits Across U.S. Operators

Food and beverage plants are the primary audience for this article, but the same recovery logic reaches the other segments around them:

planta biogas recuperacion amoniaco webp

Commercial AD & Biogas Developers

Food-waste digesters concentrate ammonia in reject water, so OTAR® at the dewatering stage protects biogas yield while adding a nitrogen revenue line.

animal farm icon

Large-scale dairy & swine CAFOs

Dairy processors with adjacent farms, or cooperatives that process their members’ milk, can close the loop by returning recovered nitrogen to the same supply chain.

municipal wastewater

Municipal wastewater treatment plants (WWTPs)

Plants that receive high-strength industrial discharges benefit when processors pretreat on-site: less nitrogen reaches the head of the works, and less aeration and chemical dosing is needed.

gestion residuos organicos recuperacion amoniaco webp

High-protein food & beverage processors

Meatpacking, dairy, seafood, fermentation and rendering plants cut surcharge exposure and can turn recovered nitrogen into an OMRI-eligible product or an offset for ammonia they already buy.

Landfill leachate icon

Solid waste & landfill operators

Operators who accept food-processing residuals alongside municipal waste see the same protein-driven ammonia in their leachate, and the same stripping approach applies.

OTAR® vs Struvite Precipitation: Choosing the Right Nutrient Recovery Technology

OTAR® vs Struvite Precipitation: Choosing the Right Nutrient Recovery Technology

Struvite mainly recovers phosphorus, while OTAR® mainly recovers nitrogen. For most high-TAN streams, the two technologies complement each other rather than compete. However, understanding the difference prevents expensive mistakes in technology selection.

Many operators of wastewater and digestate plants consider struvite precipitation for nutrient recovery. However, choosing between ammonia recovery vs struvite precipitation depends on what each technology actually removes. This article explains when struvite is the right choice and when OTAR® is preferable. It also shows how the two can work together on complex streams.

What Is Struvite Precipitation?

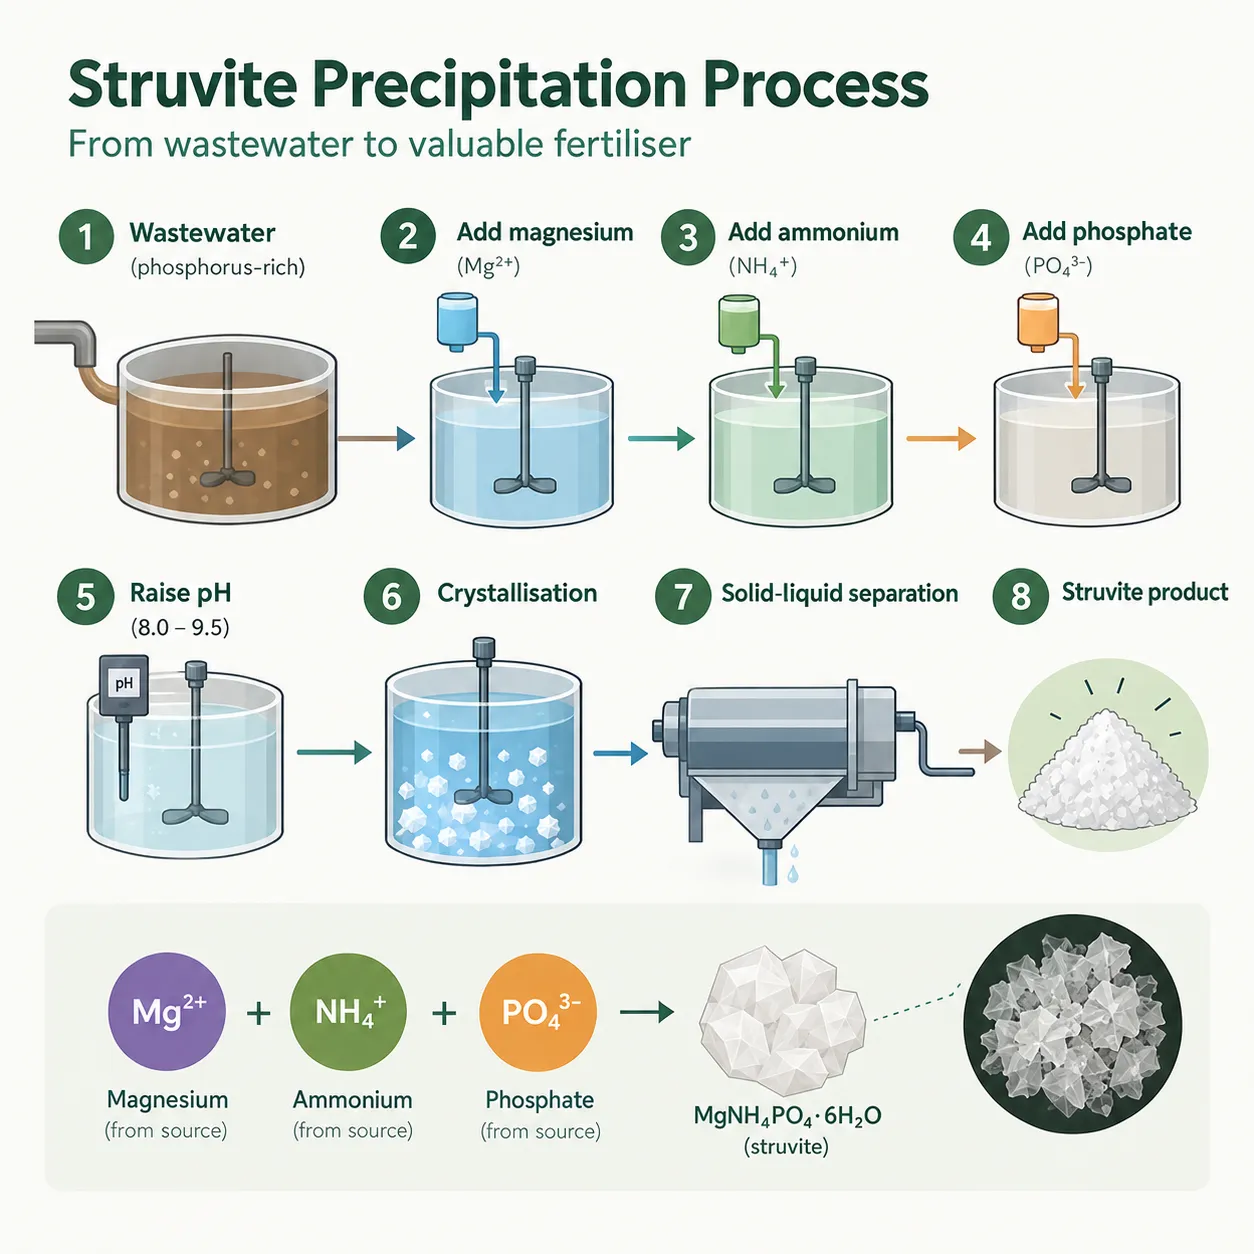
Struvite is magnesium ammonium phosphate (MgNH₄PO₄·6H₂O), a slow-release fertilizer mineral. It crystallizes when magnesium, ammonium and phosphate meet in the right proportions at elevated pH. Precipitation works best on phosphorus-rich streams, typically sewage sludge digestion liquors and food processing effluents. In addition, the product has strong agronomic properties and good market acceptance.

Struvite Precipitation Process

Where Struvite Has Limits

Struvite precipitation is primarily a phosphorus recovery technology. In a typical stream, it removes only 10 to 30% of ammoniacal nitrogen. The reason is stoichiometry, because the reaction needs equimolar phosphate.

However, most high-TAN streams carry far more nitrogen than phosphorus. Examples include digestate reject water, landfill leachate and food processing effluents. As a result, substantial ammonia remains after precipitation and needs further treatment.


When OTAR Is the Right Choice

OTAR® suits high-TAN streams regardless of their phosphorus concentration. It fits best where the main challenge is ammonia compliance or nitrogen value recovery. Moreover, OTAR® delivers 85 to 99% nitrogen removal efficiency, far above struvite. It also does so at comparable or lower cost per metric ton of nitrogen recovered. In addition, OTAR®’s modular variants adapt to the energy and product market available at each site.

TKO OTAR (5)

Combined Approaches

Some streams, such as certain sewage sludge liquors, carry both high TAN and high phosphorus. For these streams, a combined approach is often best. First, struvite precipitation recovers phosphorus and a fraction of the nitrogen. Then, OTAR® removes the remaining ammonia load. Organics USA can design integrated treatment trains for complex stream compositions. Therefore, the key is sequencing the technologies to tackle both nutrients efficiently, rather than choosing one.


Which U.S. Operators Should Consider Each Approach?

The right answer depends on your stream’s nitrogen-to-phosphorus balance and on which nutrient your permit or product market cares about most:

planta biogas recuperacion amoniaco webp

Commercial AD & Biogas Developers

Digestate reject water is typically nitrogen-heavy. OTAR® is usually the primary technology, protecting digesters from ammonia inhibition and producing a sellable ammonium product.

animal farm icon

Large-scale dairy & swine CAFOs

Manure carries both nitrogen and phosphorus, and many states apply phosphorus-based land-application limits. A combined train — struvite for phosphorus, OTAR® for nitrogen — can address both constraints and create two marketable products.

municipal wastewater

Municipal wastewater treatment plants (WWTPs)

Plants facing phosphorus limits often start with struvite on sludge digestion liquors. Because that step leaves most of the ammonia behind, OTAR® on the remaining centrate handles the nitrogen load before it returns to the head of the works.

gestion residuos organicos recuperacion amoniaco webp

High-protein food & beverage processors

Protein-rich effluents are dominated by ammoniacal nitrogen. OTAR® typically leads here, cutting surcharge exposure, with struvite added only where phosphorus is also a discharge concern.

Landfill leachate icon

Solid waste & landfill operators

Leachate carries far more nitrogen than phosphorus, so struvite offers little. OTAR® is the better fit for persistent leachate TAN.

Should I use ammonia stripping or struvite precipitation or nutrient recovery?

Choose struvite precipitation when phosphorus recovery is the main goal. In contrast, OTAR® thermal ammonia stripping suits streams where ammonia compliance or nitrogen recovery matters most. Finally, for streams with high TAN and high phosphorus, use struvite first and OTAR® second.

The OTAR Approach

OTAR (Organics Thermal Ammonia Recovery)

OTAR is a modular platform with over 20 years of operational experience and proven installations in Asia. For operators currently spending on biological nitrogen removal, the most commercially attractive configuration is Variant 2. Which is the water absorption that converts a treatment cost into ammonium hydroxide revenue with no acid supply chain, no salt production and no hazardous chemical handling. Where waste heat is unavailable, Variant 4’s heat recycling system achieves a coefficient of performance exceeding 15, making thermal stripping viable even from cold electricity.

Landfill Leachate Ammonia Treatment: A Proven Compliance Solution

Landfill Leachate Ammonia Treatment: A Proven Compliance Solution

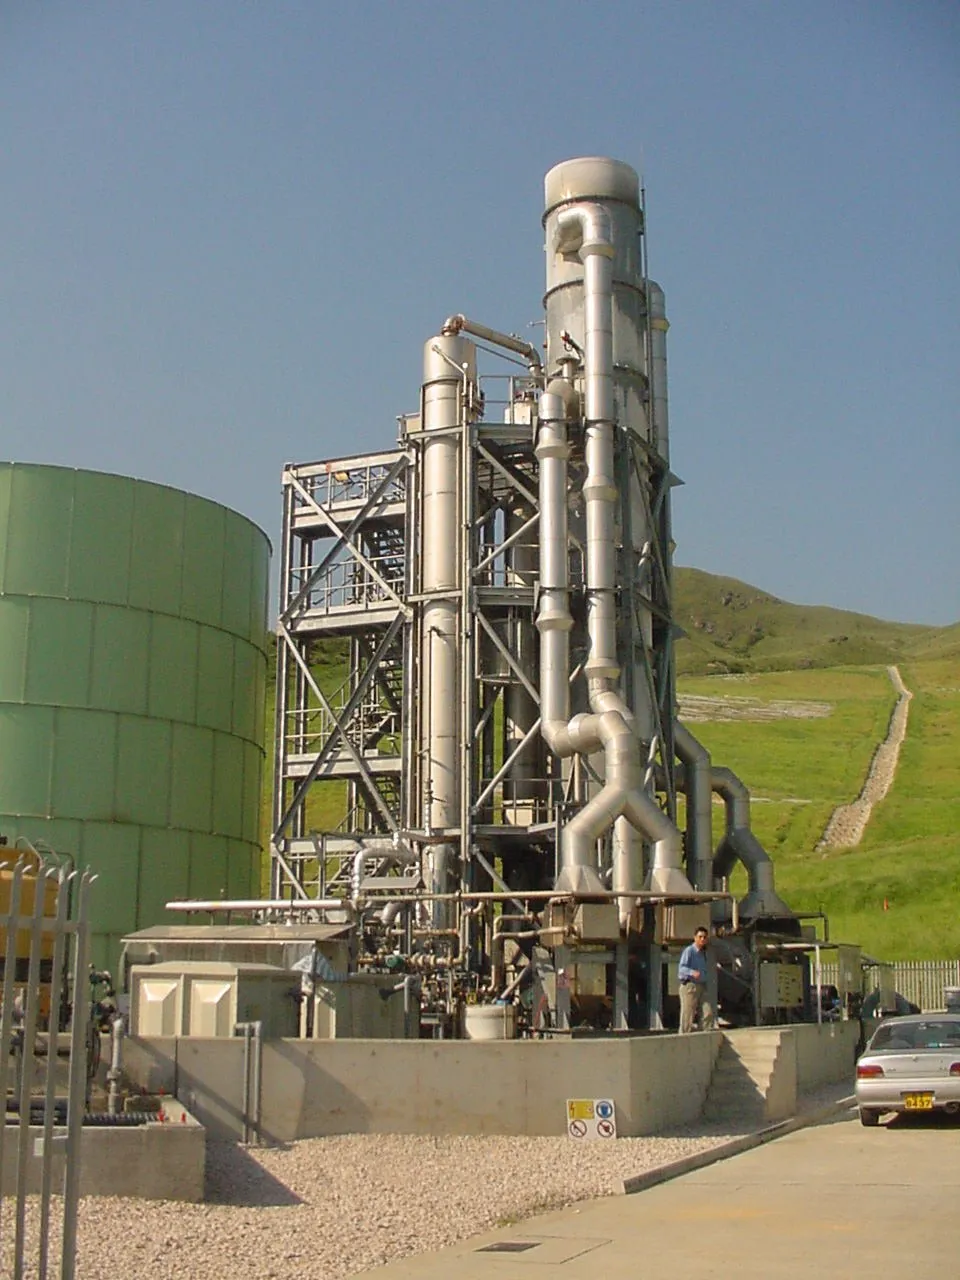
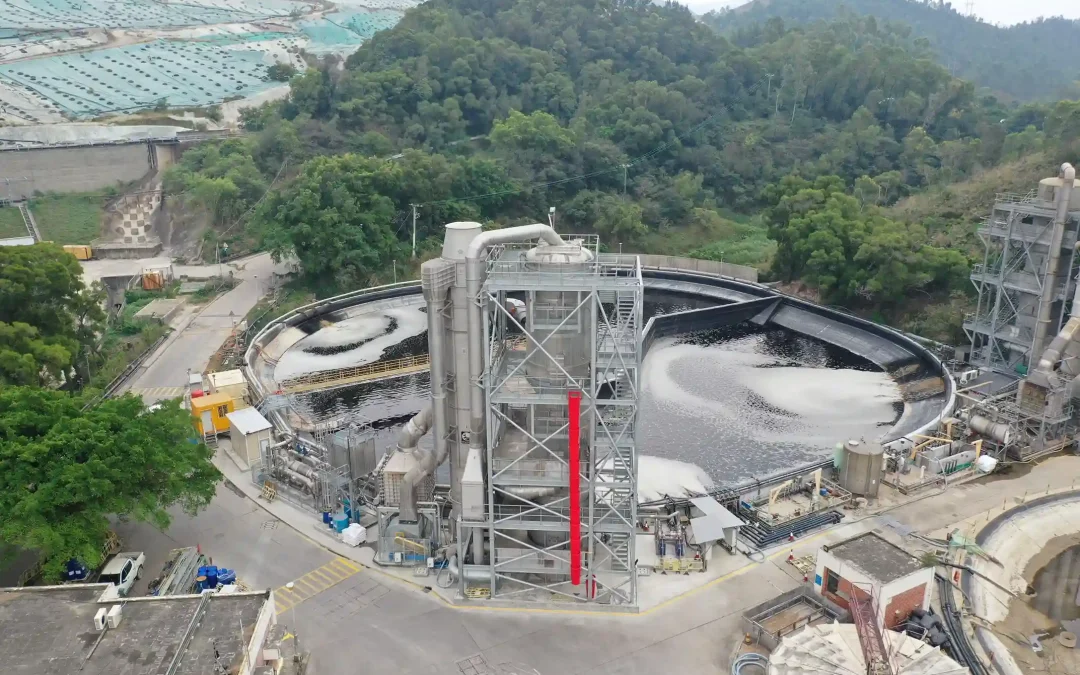
Several Hong Kong leachate treatment facilities run OTAR® Variant 1 on waste heat from landfill gas engines. As a result, they meet strict nitrogen discharge limits without handling any chemical products. It is also a proven, low-complexity approach to a notoriously difficult stream.

Landfill leachate ammonia treatment is one of the toughest challenges in waste management. However, OTAR® has solved it in real installations for more than 25 years. Below, we explain why leachate is so hard to treat and how OTAR® copes. We also cover the Hong Kong precedent and the option to recover ammonia as a product.

Why Landfill Leachate Ammonia Treatment Is Difficult

Leachate typically carries total ammoniacal nitrogen (TAN) concentrations of 1,000 to 4,000 mg/L. Some Hong Kong sites have recorded more than 6,000 mg/L. Moreover, these concentrations persist long after a landfill closes, sometimes for decades.


waste water lagoon crop

Biological nitrification is sensitive to temperature, pH and inhibitory compounds. Leachate is often cold and rich in inhibitors, including humic acids, heavy metals and volatile fatty acids. In addition, its volume and composition shift with the seasons. Keeping a stable nitrifying biomass under these conditions is very difficult. Therefore, process failures often cause permit breaches at the worst possible time.

Why Thermal Stripping Works Where Biology Struggles

OTAR® is a physico-chemical process, so temperature and pH equilibrium drive its performance, not biological activity. Inhibitors, seasonal changes in leachate composition and temperature variation within design limits thus do not affect it. Consequently, performance stays consistent and predictable throughout the year. This is especially valuable for operators with strict discharge limits or sensitive receiving waters.


The Hong Kong Precedent

The best-documented OTAR® leachate references come from a series of installations in Hong Kong. For example, the WENT landfill system has operated since 1998. Because Hong Kong has strict nitrogen limits and no local ammonia market, Variant 1 became the best fit. Variant 1 pairs waste heat with thermal destruction.

These sites draw waste heat from nearby biogas engines and landfill gas generation. Thus, they achieved full regulatory compliance without chemical handling or product marketing. Likewise, this precedent applies directly to U.S. landfill operators facing tightening discharge permit conditions, including NPDES permits and POTW pretreatment limits.

TKO OTAR (5)

The Recovery Option: When There Is a Market

When a buyer for ammonium hydroxide exists, OTAR® Variant 2 turns a compliance cost into partial revenue. Typical buyers are agricultural or industrial users. For instance, 5,000 m³ of leachate a year at 2,500 mg/L TAN holds about 12.5 metric tons of nitrogen. So, that nitrogen can yield roughly 50 to 60 metric tons of ammonium hydroxide solution a year. Operators can also start with Variant 1 and upgrade to Variant 2 once market arrangements develop. In many U.S. regions, agricultural and industrial buyers are closer at hand than in Hong Kong, which can make recovery worth evaluating from day one.


Who Else in the U.S. Faces This Ammonia Challenge?

Leachate is the hardest high-TAN stream, but the same physico-chemical logic applies across the segments Organics USA serves:

planta biogas recuperacion amoniaco webp

Commercial AD & Biogas Developers

Sites that pair landfill gas or digester biogas engines with high-TAN liquids already have the waste heat that makes OTAR® efficient.

animal farm icon

Large-scale dairy & swine CAFOs

Where operators handle similarly inhibitory, nitrogen-heavy liquids, stripping avoids the biological instability that leachate operators know well, and Variant 2 or 3 turns the ammonia into a farm-ready fertilizer.

municipal wastewater

Municipal wastewater treatment plants (WWTPs)

Plants that accept hauled or piped leachate often see it as a nitrogen shock load on their biological process. Pretreating leachate with OTAR® at the landfill, or treating the plant’s own high-strength sidestreams, protects nitrification and helps plants keep meeting NPDES nitrogen limits.

gestion residuos organicos recuperacion amoniaco webp

High-protein food & beverage processors

Protein-rich effluents can swing in strength and temperature. Because OTAR® does not depend on a living biomass, it handles those swings without the process failures that cause permit breaches.

Landfill leachate icon

Solid waste & landfill operators

Operators of active and closed landfills use thermal stripping to hold permit compliance through cold seasons and long post-closure periods, with waste heat from landfill gas engines as the natural energy source.

How do you remove ammonia from landfill leachate?

Thermal ammonia stripping removes ammonia from landfill leachate without relying on biology. OTAR® uses waste heat to strip the ammonia, then destroys it or recovers it as ammonium hydroxide. Because the process is physico-chemical, inhibitors and seasonal swings do not disrupt it. Hong Kong sites have relied on this approach for more than 25 years.

The OTAR Approach

OTAR (Organics Thermal Ammonia Recovery)

OTAR is a modular platform with over 20 years of operational experience and proven installations in Asia. For operators currently spending on biological nitrogen removal, the most commercially attractive configuration is Variant 2. Which is the water absorption that converts a treatment cost into ammonium hydroxide revenue with no acid supply chain, no salt production and no hazardous chemical handling. Where waste heat is unavailable, Variant 4’s heat recycling system achieves a coefficient of performance exceeding 15, making thermal stripping viable even from cold electricity.

Building the Business Case: OTAR® Return on Investment

Building the Business Case: OTAR® Return on Investment

OTAR®’s business case rests on three simultaneous value streams. Together, they frequently produce payback periods that compete favorably with conventional capital investment.

For most operators, the investment decision comes down to three questions: what are the value streams, what is the payback period, and what are the risks?

Value Stream 1: Reduced Treatment Costs

Every ton of ammonia that OTAR® recovers before it reaches the biological treatment system is a ton the plant no longer needs to nitrify and denitrify. The energy saving from avoided aeration is typically 3–8 kWh per kg of nitrogen removed. At current U.S. industrial electricity prices (approximately $0.07–$0.15/kWh, per EIA data), this generates a saving of roughly $0.21–$1.20 per kg N.

In practice, $210–$1,200 per ton of nitrogen diverted from biological nitrogen removal (BNR). Associated savings in carbon dosing, alkalinity supplement, and sludge disposal add further. For OTAR®’s Variant 4 (heat recycling), the system’s coefficient of performance exceeds 15. Therefore, the electrical energy needed to drive stripping is far smaller than the treatment cost it avoids.

OTAR value stream (2)

Value Stream 2: Product Revenue

Recovered ammonium hydroxide (Variant 2) or ammonium sulfate (Variant 3) generates a direct revenue stream. For Variant 2, standard-grade ammonium hydroxide solution typically achieves $200–$380 per ton in established markets. OMRI-certified product commands a premium above this range.

For a system recovering 90 tons of nitrogen per year as ammonium hydroxide, net product revenue typically contributes $54,000–$120,000 per year. This depends on product grade and offtake terms. In some cases, the product even replaces purchased inputs within the same facility. For example, one chemical manufacturing plant reduced its ammonium hydroxide purchases by nearly a third — a directly measurable saving.

OTAR value stream (1)

The OTAR Approach

OTAR (Organics Thermal Ammonia Recovery)

OTAR® (On-Site Thermal Ammonia Recovery) is a modular platform with over 20 years of operational experience and proven installations across Asia and the UK, with growing adoption across the United States. For operators currently spending on biological nitrogen removal, Variant 2, water absorption, is usually the most commercially attractive option. It converts a treatment cost into ammonium hydroxide revenue, with no acid supply chain, no salt production, and no hazardous chemical handling. Where waste heat isn’t available, however, Variant 4’s heat recycling system still achieves a coefficient of performance exceeding 15, making thermal stripping viable even from cold electricity.

Value Stream 3: Capacity and Compliance Benefits

Diverting ammonia from the main treatment stream before it enters BNR frequently unlocks latent treatment capacity. As a result, facilities can accept higher loads or additional feedstocks without capital investment in new infrastructure. In addition, OTAR®’s physico-chemical process — unlike BNR — resists inhibitors, temperature fluctuations, and biomass instability.

Consequently, it delivers more reliable permit compliance, which matters most for facilities with tight NPDES discharge limits or sites in watersheds subject to state nutrient reduction requirements or EPA-mandated Total Maximum Daily Load (TMDL) programs.

OTAR value stream (3)

Indicative Payback: A Worked Example

OTAR AD site 1

Site: AD plant, 30,000 tpa food waste.

Reject water: 20,000 m³/year at 3,200 mg/L TAN.

Recoverable nitrogen: 64 tonnes N/year.

OTAR configuration: Variant 2 (waste heat available from gas engine).

Indicative capital cost: : $510,000–$650,000

Annual OTAR operating cost: : $40,000–$54,000.

Annual gross benefit (energy saving + ammonium hydroxide revenue + capacity value): $160,000–$215,000.

Net annual benefit: $115,000–$160,000

Simple payback: 4–5 years.

These figures are indicative, since actual values depend on stream characteristics, waste heat availability, energy prices and product offtake terms. However, the Organics USA can provide a site-specific assessment.